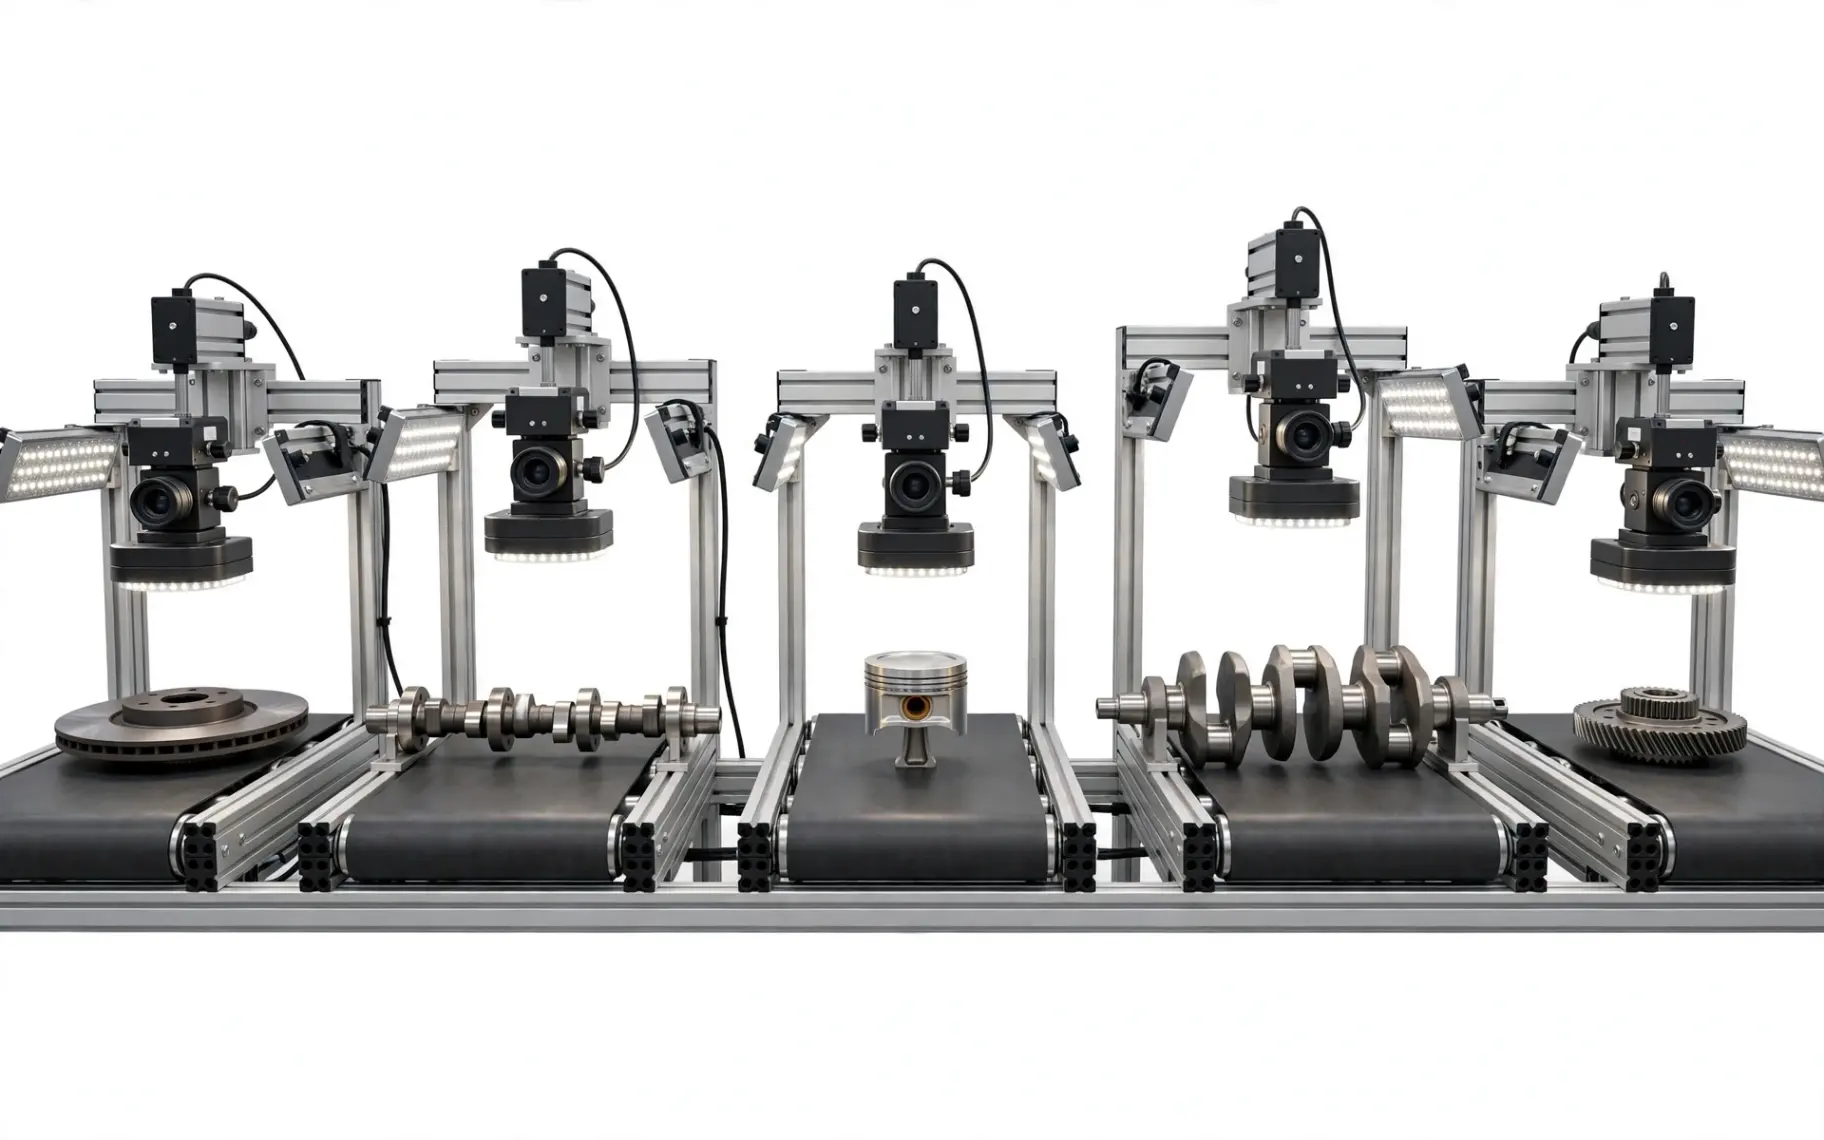
Automotive Machine Vision Inspection System
Machine Vision Solutions for Automotive Component Inspection
Automotive manufacturing involves multiple inspection points where component identity, quantity and assembly condition must be verified. An automotive machine vision inspection system can detect visible issues such as incorrect part variants, missing fasteners, marking errors and incomplete assemblies. It can also check component orientation and product markings at selected production stages.
Orchid Technology provides industrial machine vision solutions for automotive inspection applications. Each solution can be tailored to the component design, production process and quality requirements, helping manufacturers incorporate automated visual checks into their workflows.
How Does Automotive Machine Vision Inspection Work?
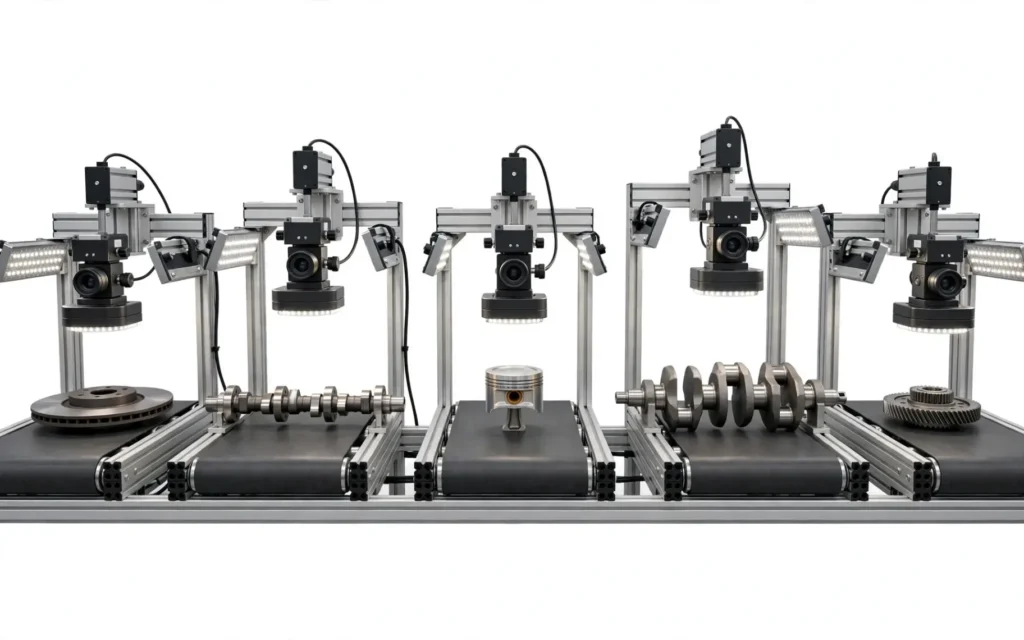
A machine vision inspection process begins by capturing images of a component or assembly at a defined inspection point. Industrial cameras, suitable lenses and controlled lighting are selected according to the part’s surface, shape, markings and inspection environment.
Image-processing software then examines the captured information for specified features. Depending on the application, it may identify a component type, locate a marking, count visible parts, check component presence or compare an assembly against predefined visual requirements.
The inspection result is evaluated against configured acceptance criteria. The system can communicate a result to the connected production equipment or control system, where the application supports this integration. Depending on the process design, results can be used for operator alerts, production records or rejection handling.
This approach supports automated visual inspection in automotive manufacturing by applying repeatable inspection rules to defined tasks. The inspection method and achievable accuracy depend on camera placement, lighting, component variation, image quality and the validation of the complete application.
Why Use Machine Vision in Automotive Manufacturing?
Automotive production includes many checks that depend on recognising the correct part, confirming that a feature is present or verifying that an assembly matches its intended configuration. A machine vision quality control system can help perform these checks consistently at selected production stages.
An automated automotive inspection system can support manufacturers by:
Identifying incorrect component variants before further processing.
- Checking the presence of selected parts and assembly features.
- Reading or verifying visible product markings.
- Counting components against predefined quantity requirements.
- Detecting specified placement and orientation differences.
- Producing inspection results for connected production systems.
- Reducing dependence on repetitive manual visual checks.
For automotive suppliers handling multiple part numbers, an automated quality inspection system for automotive parts can be configured around the visual differences that matter to each application. Inspection criteria should be defined and validated for the intended parts, operating conditions and acceptable defect limits.
Automotive Machine Vision Inspection Applications
Automotive Part Counting System
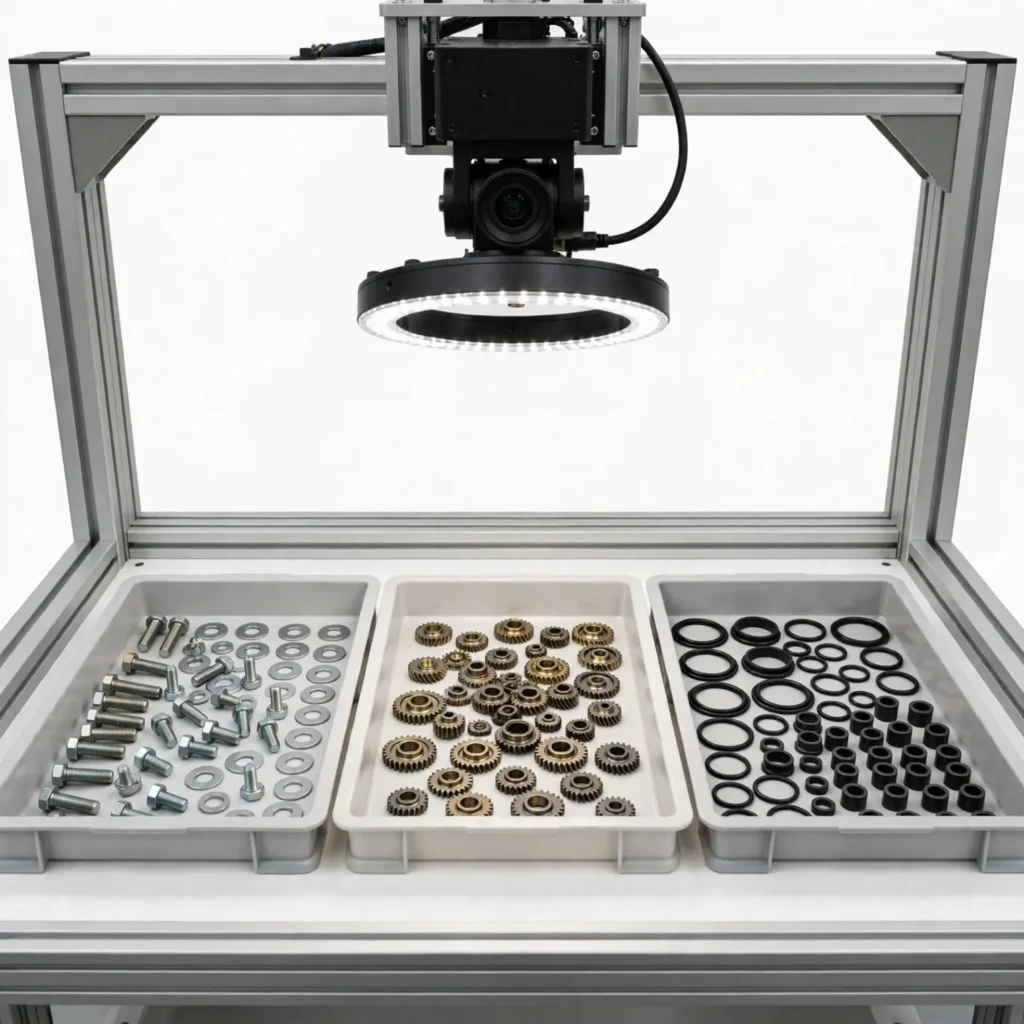
An automotive part counting system identifies and counts visible components within a defined inspection area. It can be used where manufacturers need to verify component quantities before packing, assembly, transfer or dispatch.
The vision application is configured to distinguish the required parts from the surrounding scene and compare the detected count with a specified quantity. Part overlap, orientation and background variation must be considered during system design.
Identification requirements vary by product and production process. For an example of product identification in tyre manufacturing, explore our tyre identification system
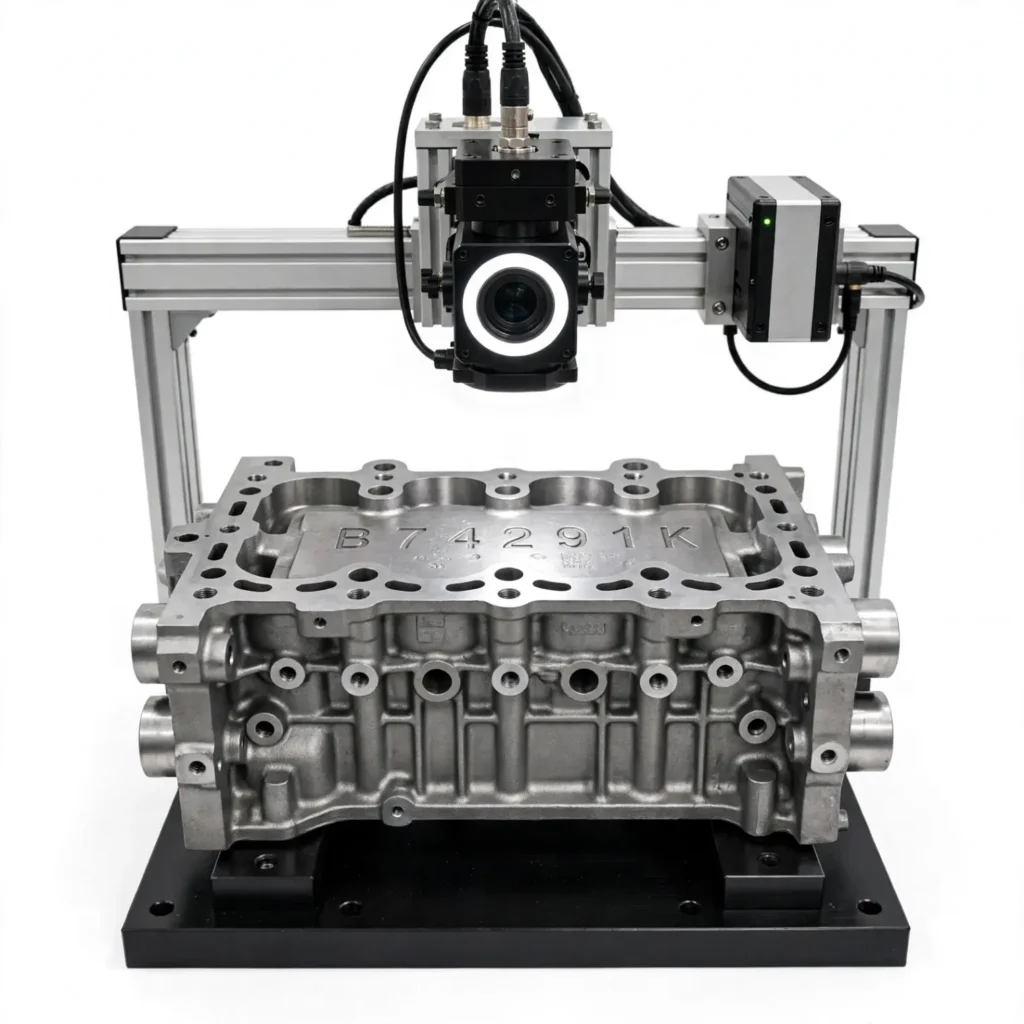
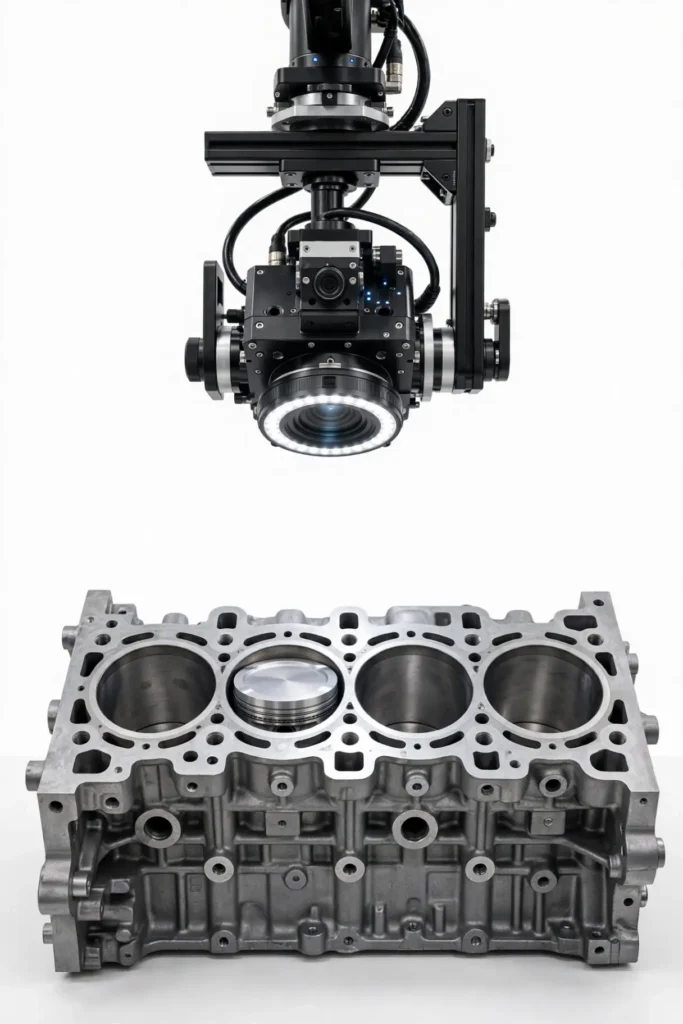
Engine Block Stamping Inspection
Engine block stamping inspection checks selected stamped, embossed or marked areas on an engine block. A vision system can examine defined characters, symbols or marking features to identify missing, inconsistent or incorrectly presented information.
Where the marking is suitable for optical character recognition, OCR inspection can be configured to read the text and compare it with expected information. The result depends on marking depth, contrast, surface finish and image quality. Marking verification can be part of a wider product identification process. See our Tyre Traceability System for an example of identification and traceability requirements in tyre manufacturing.
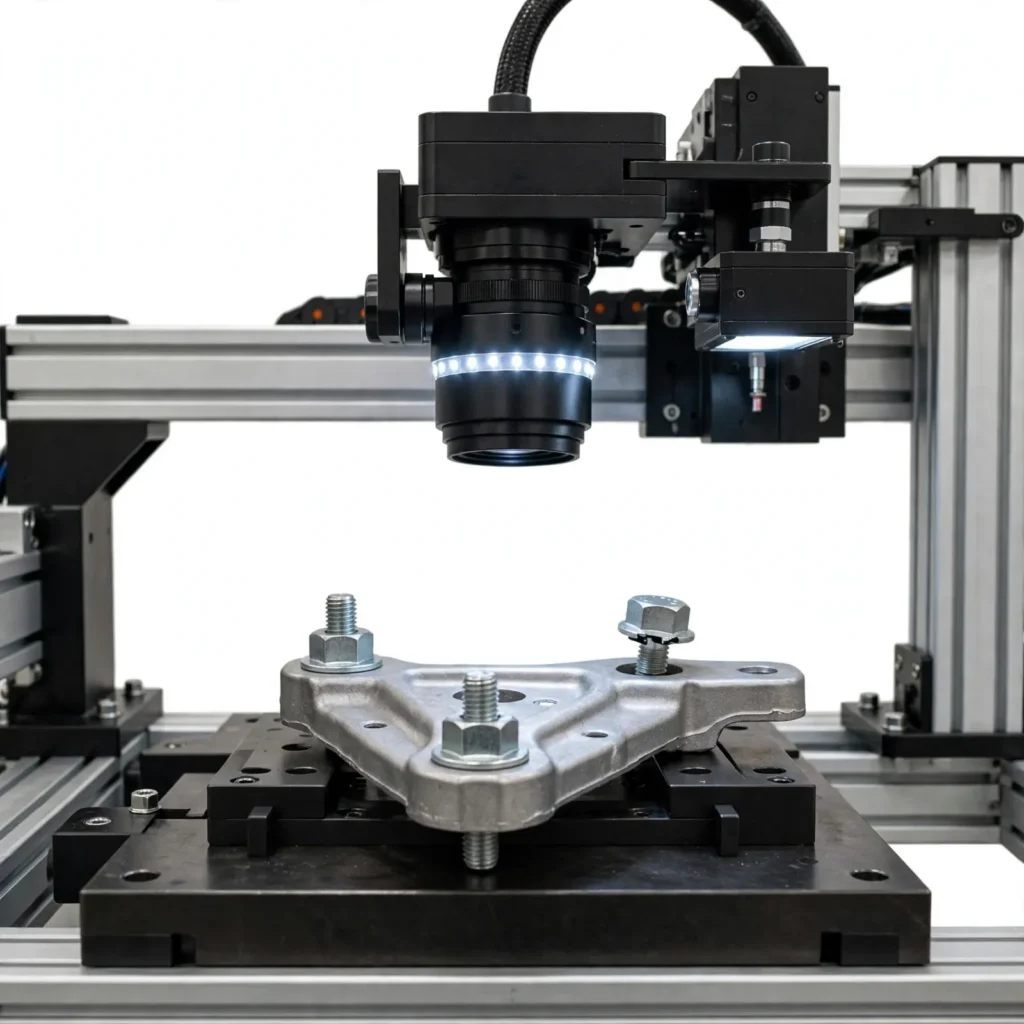
Screw Tightening Verification System
A screw tightening verification system based on machine vision checks visible conditions associated with fastener installation. Depending on the assembly, it may verify screw presence, position, head type or a specified visible seating condition.
These checks can help identify selected assembly discrepancies. However, ordinary visual inspection does not directly measure tightening torque or clamping force. Where torque confirmation is required, the vision system should be combined with appropriate tightening-tool data or a validated torque measurement method.
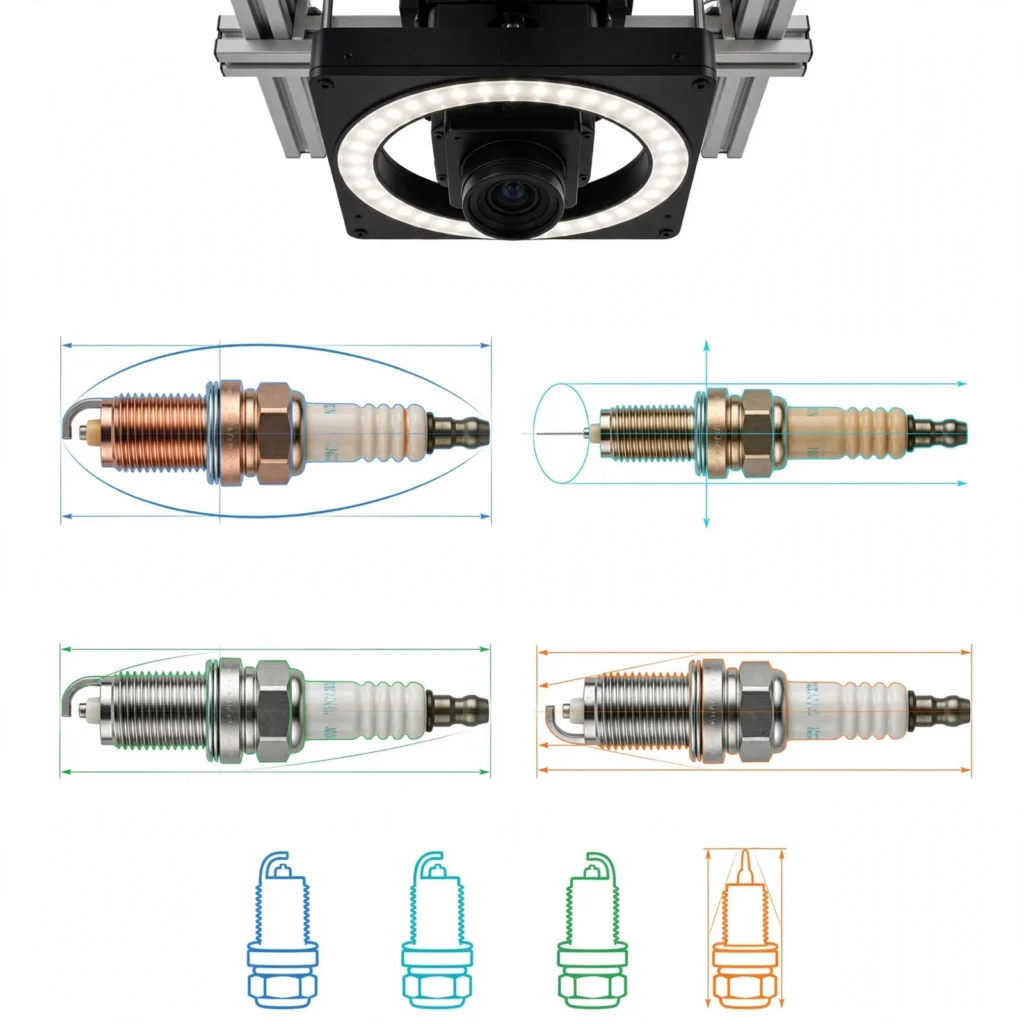
Spark Plug Type Detection System
A spark plug type detection system distinguishes between specified spark plug variants using visible characteristics such as shape, dimensions, terminal configuration or other identifiable features.
Machine vision inspection for spark plugs can help confirm that the intended variant is supplied to a workstation or placed in the correct assembly location. Reliable differentiation requires clearly identifiable features and representative images of the relevant product variants.
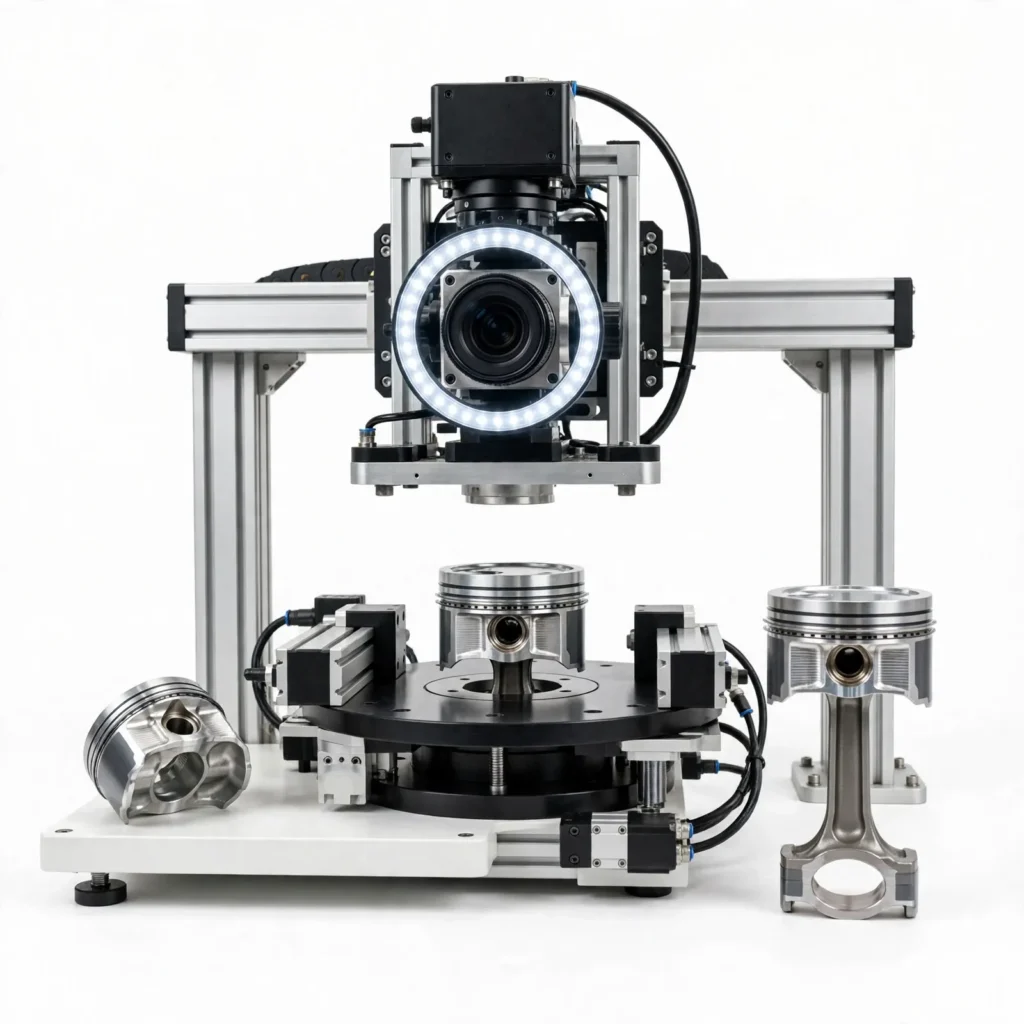
Automated Piston Inspection
An automated piston inspection system checks selected visual characteristics to distinguish piston types or verify defined features. Depending on the inspection requirement, these may include visible geometry, surface features, markings or differences between product variants.
The system compares the captured image with the configured identification criteria and reports whether the observed piston matches the expected type. Precision dimensional acceptance requires suitable calibrated measurement methods and validated tolerances.
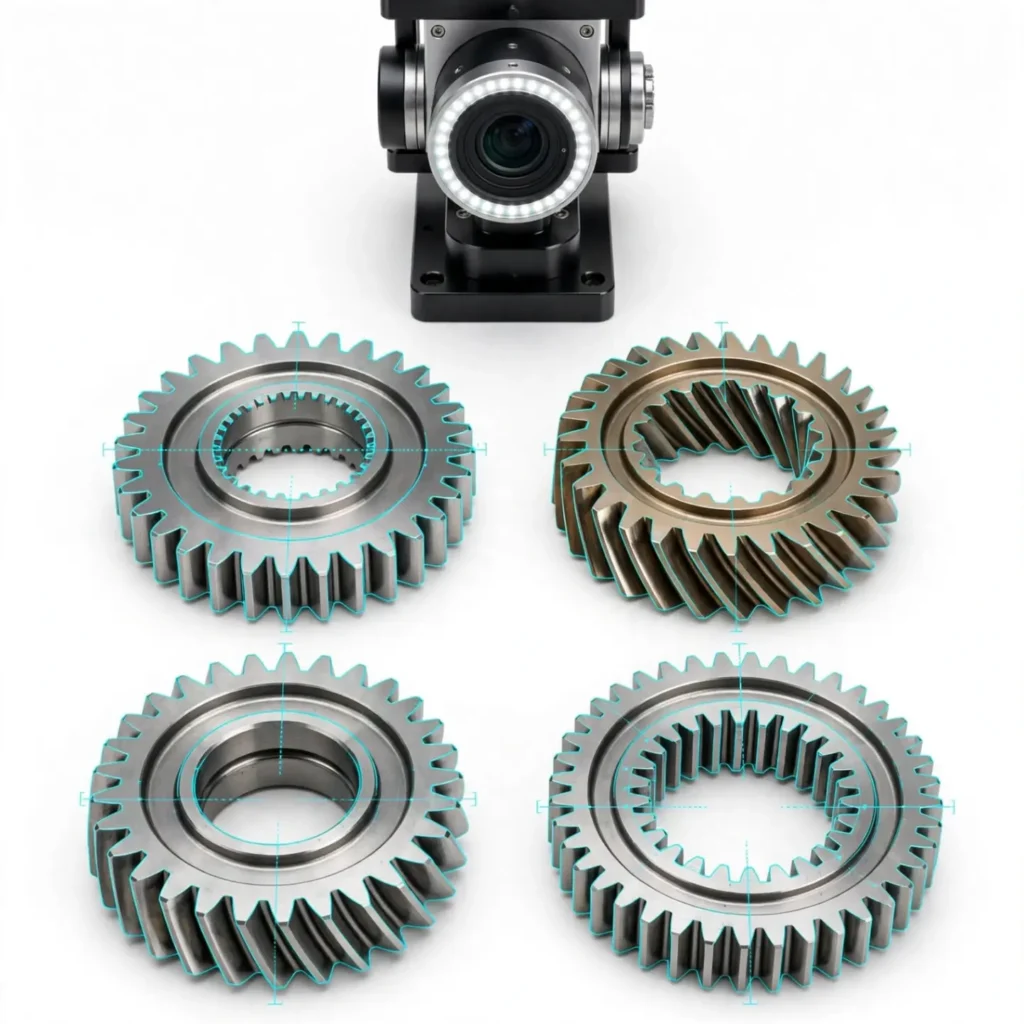
Gear Type Identification System
A gear type identification system recognises specified gear variants through their visible profile, shape, tooth arrangement or other distinguishing features. It can support component selection and verification where similar-looking gears are used across different assemblies.
The inspection setup should account for gear orientation, reflections, overlapping components and the visual differences between accepted variants. Machine vision can identify defined types when those differences are reliably observable.
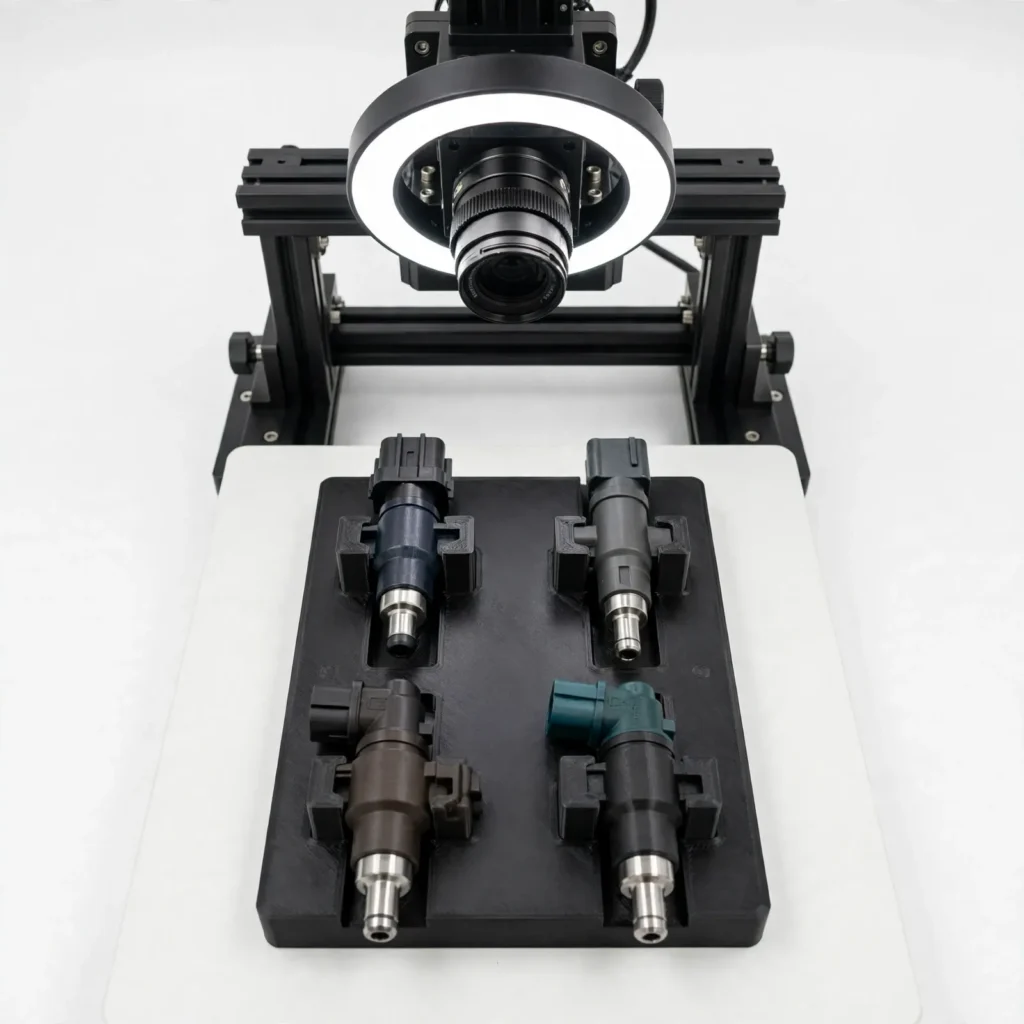
Fuel Injector Type Detection
Fuel injector type detection verifies the identity of selected injector variants before installation or during component handling. A machine vision system can inspect visible body geometry, connector arrangements, markings or other distinguishing features.
For automotive component suppliers working with multiple injector models, the inspection criteria can be configured to identify the required variant and flag a mismatch. Internal condition, fuel flow and electrical performance require separate testing methods.
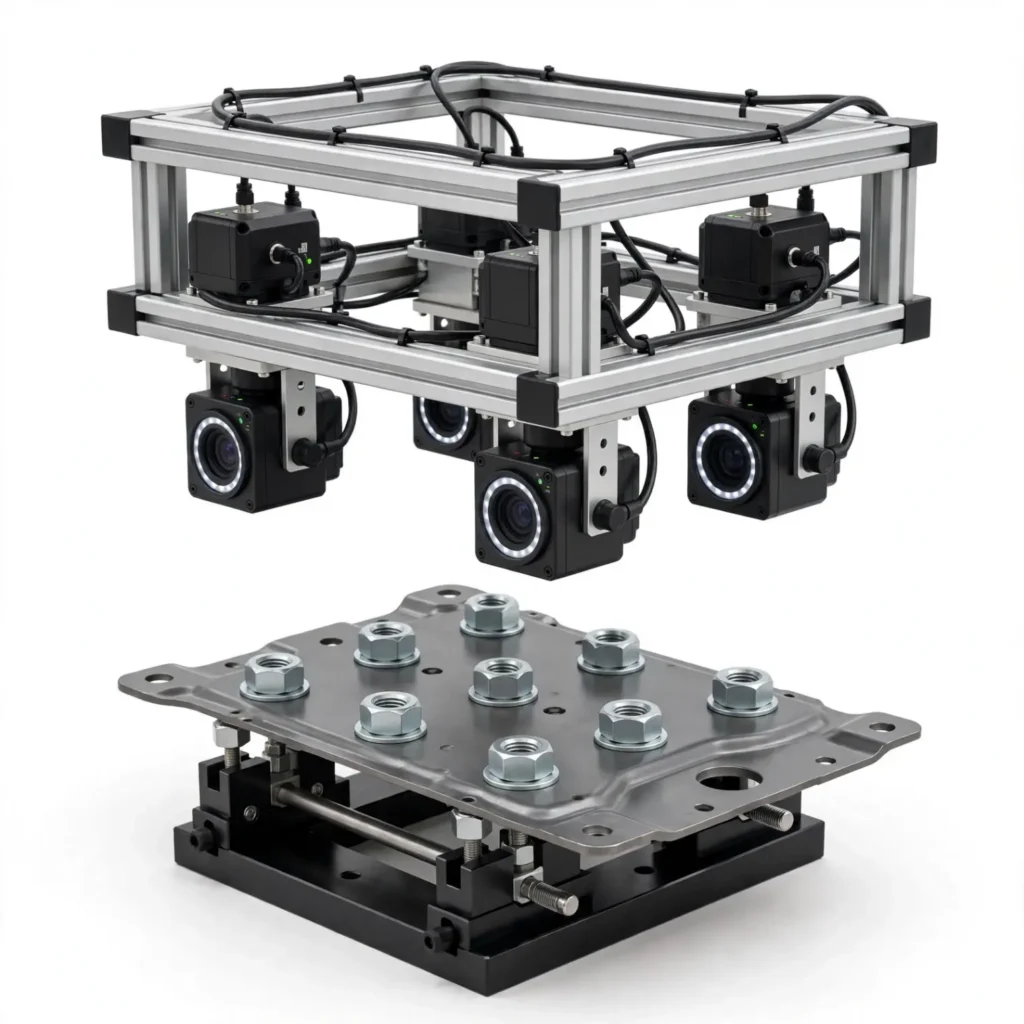
Multi-Point Nut Inspection System
A multi-point nut inspection system examines defined positions or visible features associated with nuts in an assembly. The application may check whether specified nuts are present and whether their visible positions or types match the inspection requirements.
By checking multiple locations within one image or inspection sequence, the system can help identify missing or incorrectly positioned fasteners. Hidden features and tightening force cannot be confirmed through ordinary visual inspection alone.
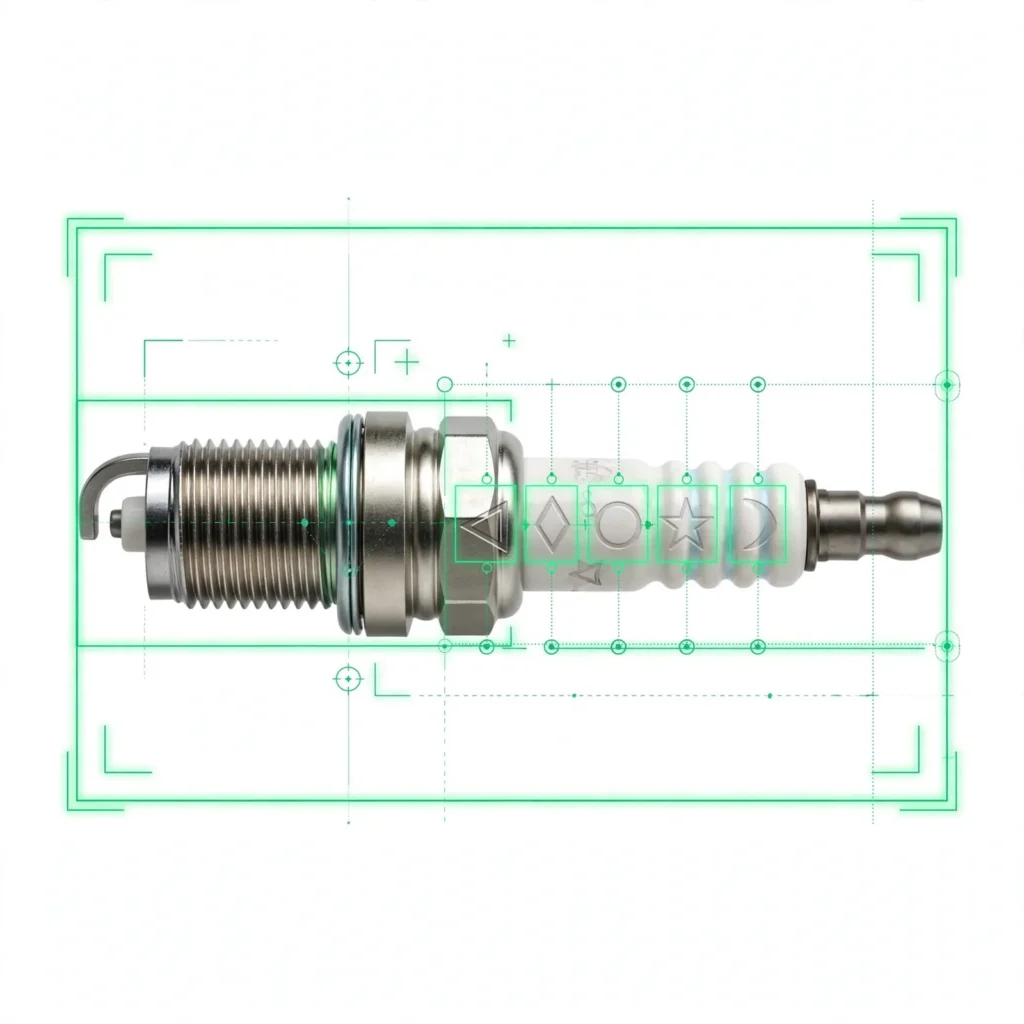
Spark Plug Marking and OCR Inspection
Spark plug marking inspection focuses on visible identification details, including specified characters, codes, symbols or product markings. An OCR inspection system for automotive components can read supported text and compare the result with an expected value.
This application can help identify missing, unreadable or incorrect markings where the characters are sufficiently clear for reliable processing. Marking material, contrast, curved surfaces and character quality should be assessed during feasibility testing.
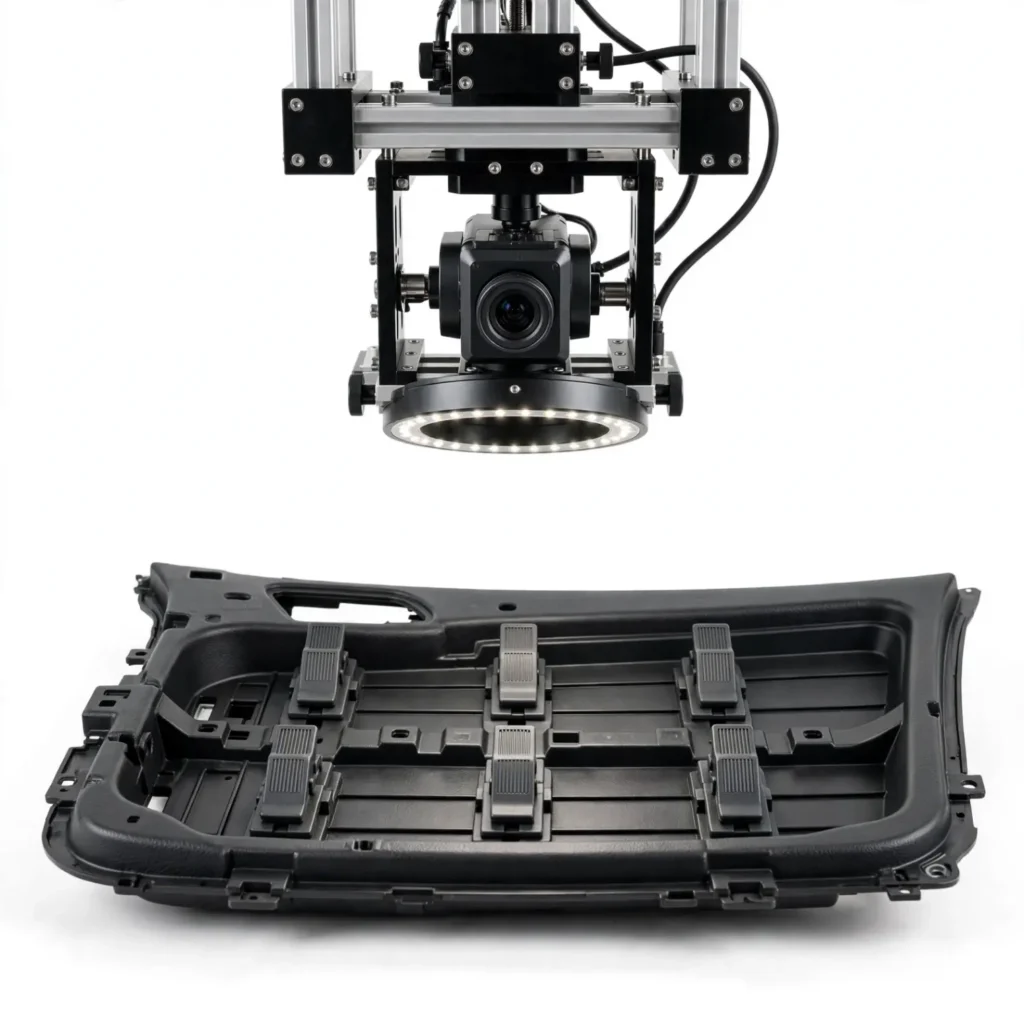
Automotive Interior Clip Presence Detection
Automotive clip presence detection checks whether specified clips are installed at designated positions in interior components. These checks can be useful for trim panels and other assemblies where small fastening elements may be difficult to verify consistently by eye.
The machine vision application examines defined clip locations and reports missing or visibly misplaced clips. Camera angle, clip colour, shadows and partial obstruction need to be considered to distinguish installed clips from similar background features.
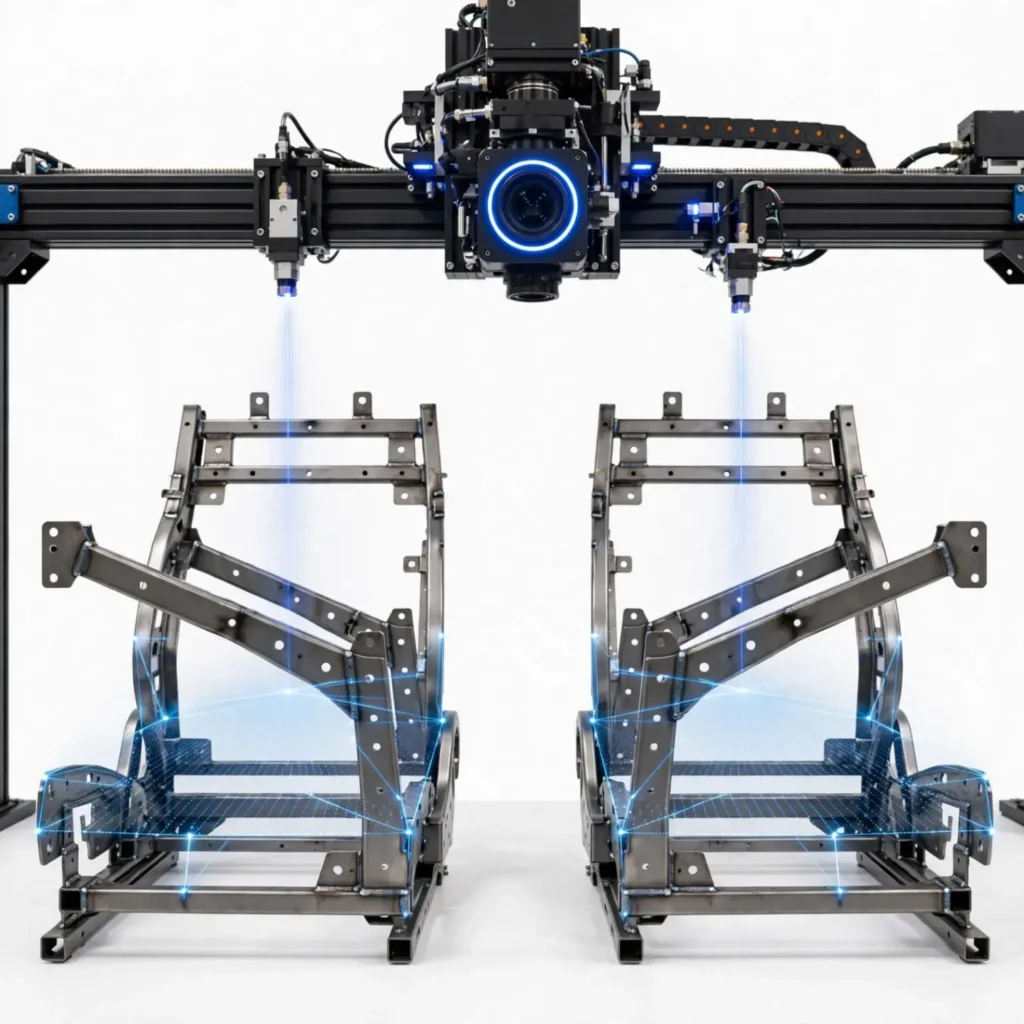
Left-Right Seat Frame Verification
An automotive part orientation inspection system can distinguish between left-hand and right-hand seat frame variants. The vision application evaluates selected shape differences, mounting features or other visible characteristics associated with each version.
This check helps confirm that the correct seat frame is supplied to the intended assembly operation. The inspection should use validated reference features that remain distinguishable across normal manufacturing variation.
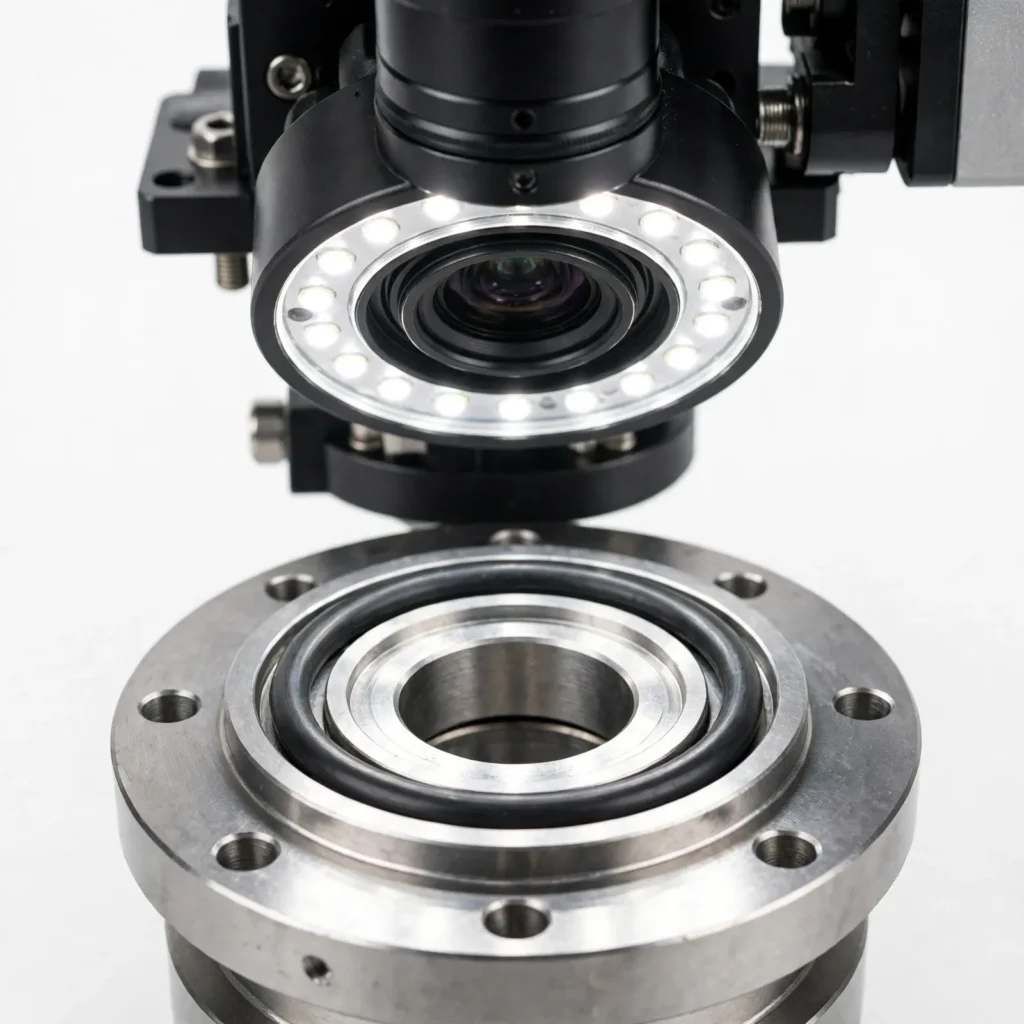
O-Ring Presence Detection System
An O-ring presence detection system checks for the presence of an O-ring at a specified component location. Depending on the part design and viewing conditions, the system may also inspect visible placement or detect selected positioning discrepancies.
O-ring inspection is particularly relevant when a missing seal could lead to a downstream assembly or quality issue. Detection reliability depends on the seal’s material, colour, dimensions, lighting and visibility against the surrounding component. For applications involving visible rubber-part features and component presence, explore our rubber component inspection solution.
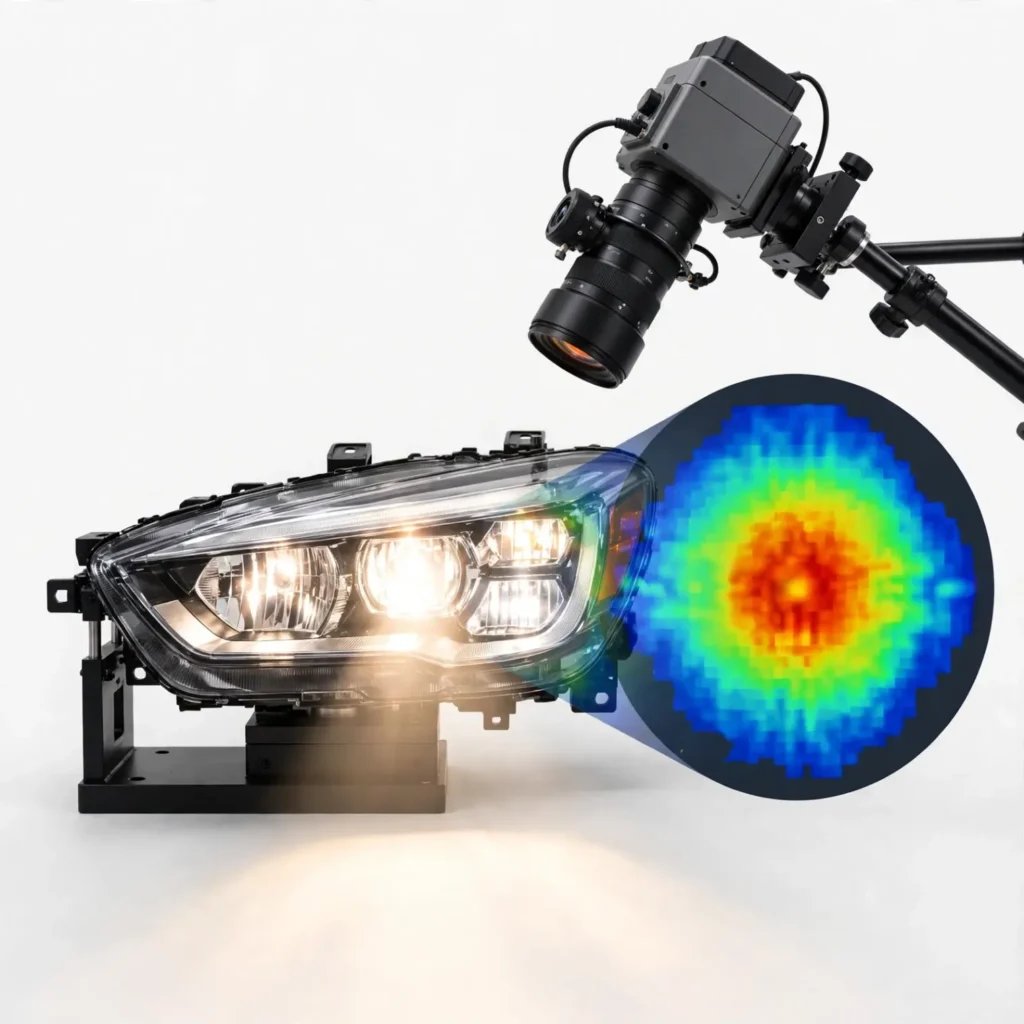
Automotive Headlight Illumination Inspection
Automotive headlight illumination inspection evaluates selected visible lighting characteristics under a defined test setup. Depending on the requirement, a vision-based arrangement may inspect whether a light source illuminates, whether specified lighting regions are visible or whether a defined visual pattern is present.
Applications requiring beam intensity, distribution, alignment or regulatory photometric measurements need suitable validated optical or photometric equipment. A standard camera-based visual check should not be treated as a replacement for certified headlight testing.
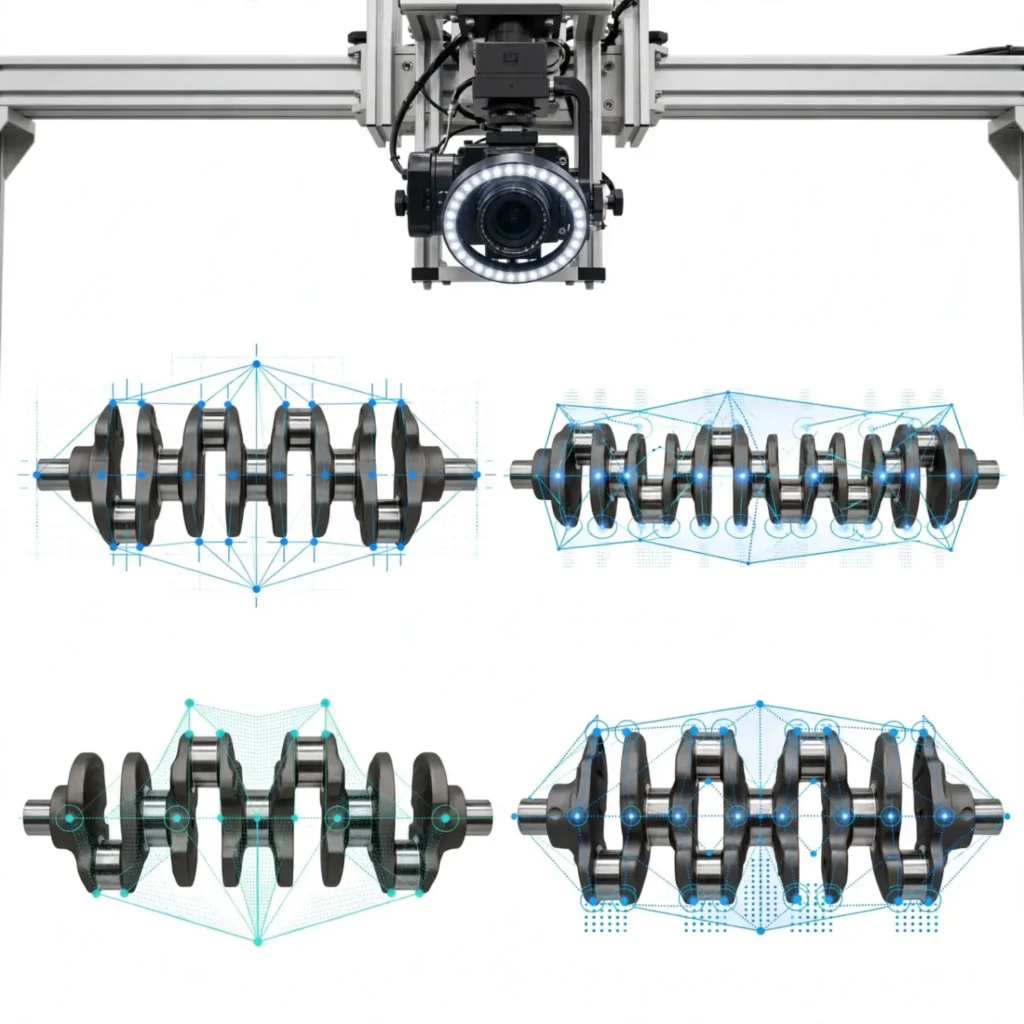
Crankshaft Type Detection
A crankshaft type detection system identifies specified crankshaft variants through visible structural features, geometry or other distinguishing characteristics. It can be applied where multiple crankshaft types are handled within the same manufacturing environment.
The system compares observed features with the defined identification criteria and reports a match or mismatch. Accurate identification depends on the visibility of distinguishing features and the control of part positioning during image capture.
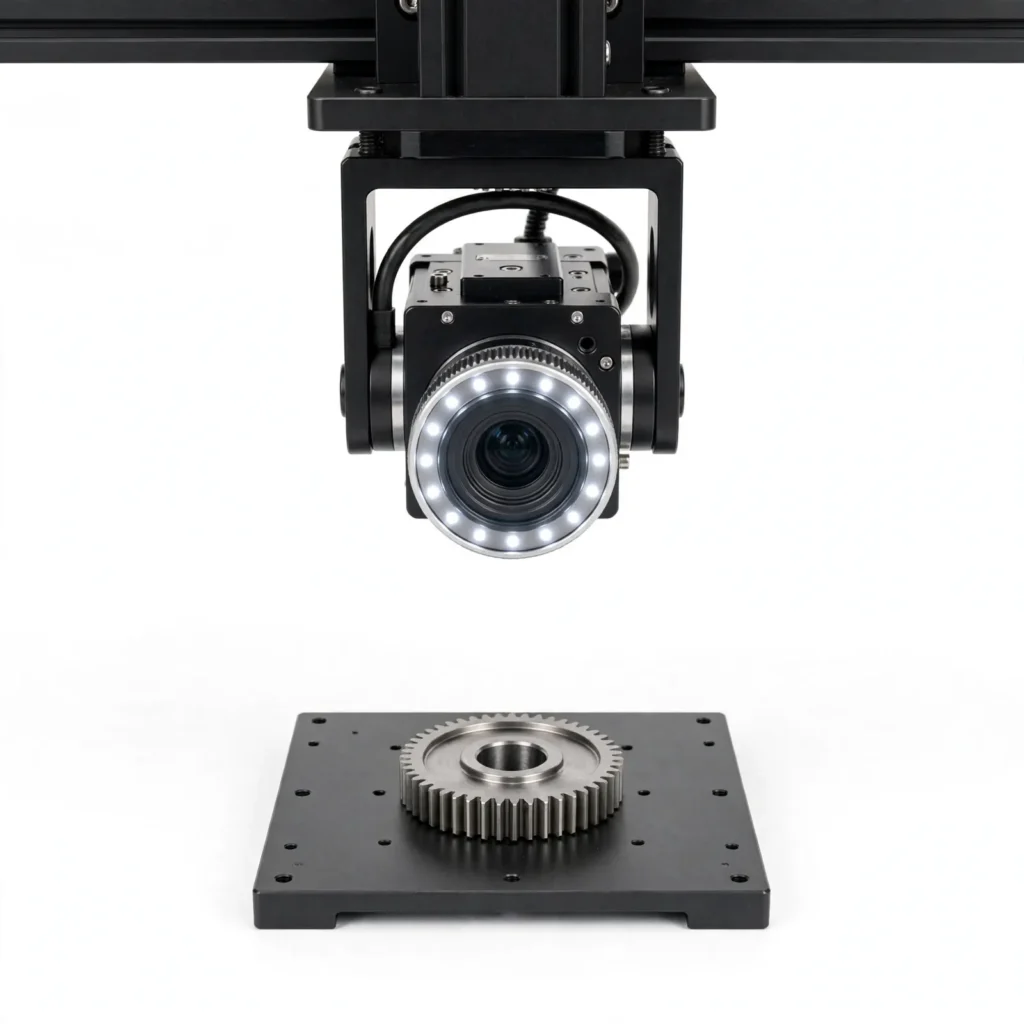
Gear Size and Dimensional Inspection
A gear size inspection system examines selected gear dimensions or size-related features using an appropriate imaging arrangement. Depending on the application, it may compare visible measurements against configured limits or distinguish gear variants based on measurable characteristics.
Automated gear dimension inspection requires suitable calibration, controlled image acquisition and validation against the specified tolerances. Critical dimensions that cannot be reliably measured using the chosen camera setup may require dedicated metrology equipment.
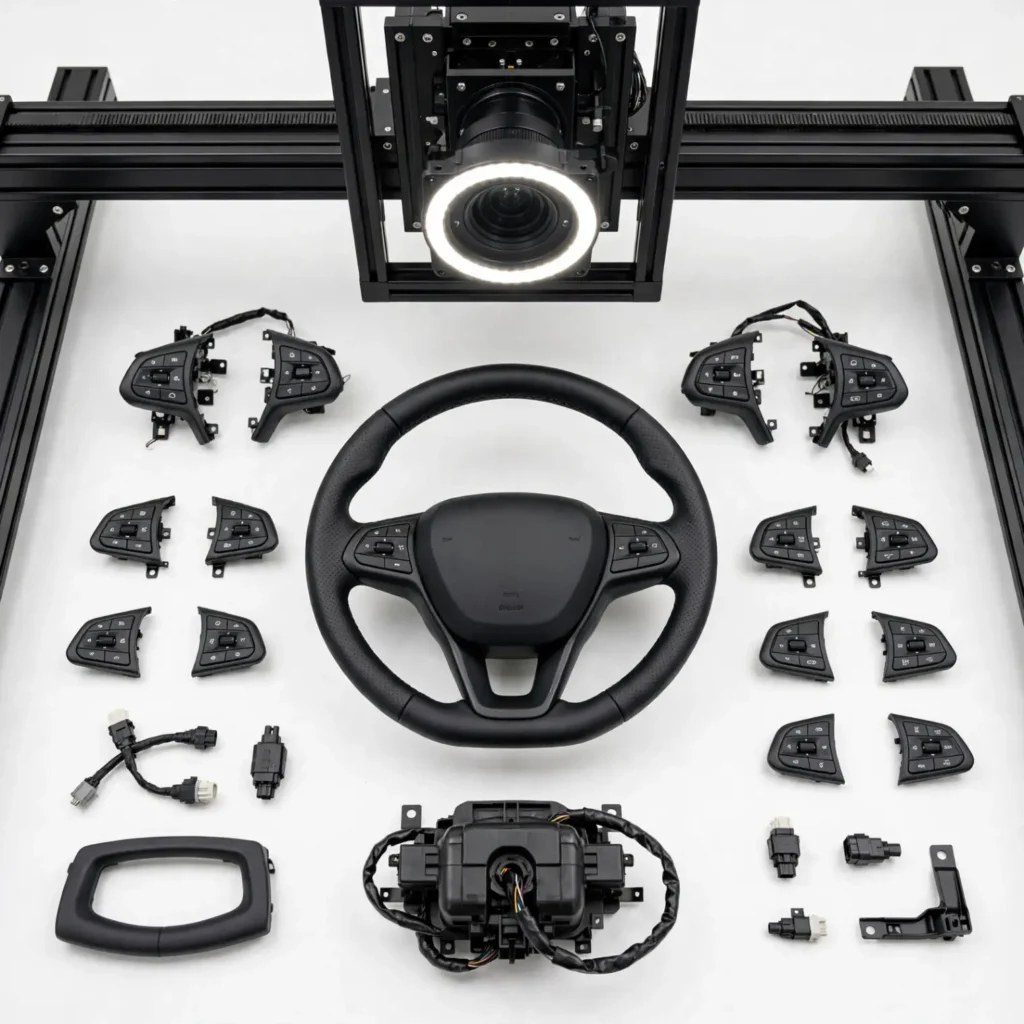
Steering Wheel Assembly Inspection
A steering wheel assembly inspection system checks selected visible components and assembly features on a steering wheel. Depending on the design, this may include component presence, placement, variant identification or confirmation that defined assembly positions are occupied.
The inspection criteria can be tailored to the required assembly configuration. Visual verification can identify observable discrepancies, while electrical operation, airbag functionality and other safety-critical functions require separate appropriate tests.
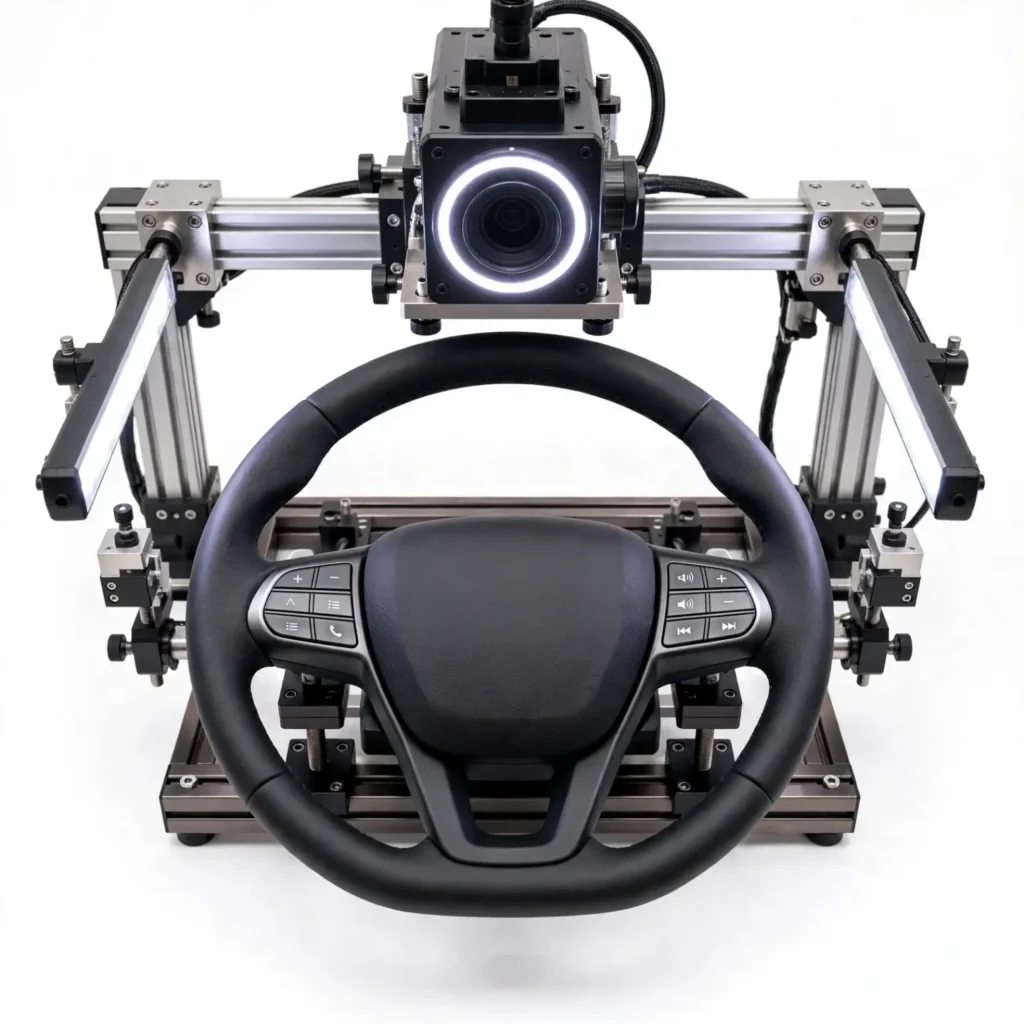
Steering Wheel Button Assembly Inspection
A steering wheel button assembly inspection system verifies the presence and arrangement of specified buttons or control components. The system can compare visible button positions and configurations with a reference layout to identify missing, misplaced or incorrect components.
This application supports automotive assembly error detection before the steering wheel moves to the next process. Button illumination, electrical connectivity and functional response must be checked separately when those characteristics form part of the quality requirement.
Discuss Your Automotive Inspection Application
Looking to automate component identification, part counting, marking verification or assembly inspection? Orchid Technology offers machine vision solutions tailored to automotive manufacturing requirements.
Share your inspection needs with our team to explore a suitable vision system for your production process and quality checks.
How Machine Vision Supports Automotive Component Inspection
An automotive machine vision inspection project generally follows a sequence of application-specific steps:
1.
Inspection Requirement Definition
2.
Image Acquisition
3.
Feature Detection and Identification
4.
Inspection Against Defined Criteria
5.
Result Classification
6.
Production-System Communication
7.
Application Validation
Key Capabilities of an Automotive Machine Vision System
The inspection functions available depend on the component, imaging conditions and validated application design.
| Inspection Capability | Typical Use |
|---|---|
| Part identification | Distinguishing component types and variants |
| Component counting | Checking visible quantities |
| Presence detection | Finding missing clips, seals or fasteners |
| Marking inspection | Examining characters, codes and symbols |
| OCR-based verification | Reading supported printed, etched or stamped text |
| Position verification | Checking defined component locations |
| Orientation checking | Distinguishing left-right or directional variants |
| Assembly verification | Checking selected visible assembly features |
| Image-based measurement | Measuring supported features with suitable calibration |
Where Are Automotive Machine Vision Solutions Used?
Automotive component manufacturing and machining
Engine and powertrain component production
Gear, piston and crankshaft manufacturing
- Seat frame and interior component assembly
- Steering wheel and control assembly
- Fastener and seal verification
- Component identification and sorting
- Marking and traceability-related inspection
- End-of-line visual quality checks
Benefits of Automotive Machine Vision Inspection
A properly configured automotive machine vision inspection system can provide practical benefits across selected manufacturing operations.
Repeatable visual checks
Applies defined inspection criteria to each inspected part.
Earlier discrepancy detection
Identifies specified visible issues before downstream processing.
Component variant verification
Helps distinguish between similar-looking automotive parts.
Assembly completeness checks
Verifies selected component and fastener positions.
Automated identification
Supports reading and checking suitable product markings.
Production data availability
Enables inspection results to be communicated to connected systems where configured.
Reduced reliance on manual checks
Supports repetitive inspection tasks at defined production points.
Application-specific inspection
Allows criteria to be tailored to the component and quality requirement.
Actual inspection performance depends on the application, visible component features and the conditions under which images are captured.
Automotive Machine Vision Solutions by Orchid Technology
Orchid Technology works with industrial machine vision and automation applications for manufacturers, OEMs and machine builders. Automotive inspection requirements can vary considerably, from identifying similar component variants to checking the presence of small assembly features or reading product markings.
Our approach begins with understanding the part, the inspection objective and the production conditions. Based on this assessment, a suitable imaging and processing arrangement can be evaluated for the required task. Where necessary, machine vision can form part of a wider automation setup involving production controls and inspection-result communication.
Explore our Machine Vision Solutions to learn more about industrial vision applications. You can also review our Success Stories for examples of application-focused automation work.
If you are evaluating an automotive component inspection system, share the component details, inspection points and expected production conditions with Orchid Technology to discuss a suitable approach.